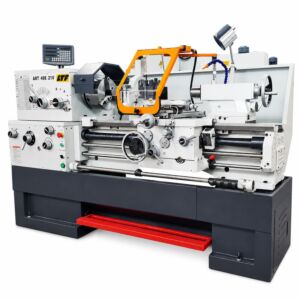
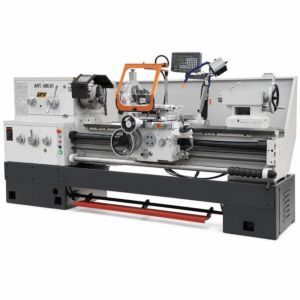
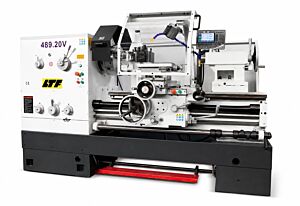
LTF precision centre lathes are conventional machine tools designed for accurate machining of mainly cylindrical, tapered, threaded or profiled components. The headstock spindle rotates the securely clamped workpiece while a cutting tool held in the tool post travels longitudinally, transversely or along a defined inclined path. Controlled interaction between spindle speed, tool feed and depth of cut removes material to produce diameters, lengths, shoulders, tapers and surface finishes in accordance with the component drawing.
The term centre or parallel lathe refers to the carriage travelling along the bedways parallel to the spindle axis. “Precision” indicates a construction focused on geometric control, stability and machining repeatability. These results depend not only on the machine but on the complete system comprising the bed, headstock, spindle, workpiece, workholding equipment, tool, carriage, tailstock, cutting parameters and measurement method.
The category includes LTF precision centre lathes with different dimensions, capacities and configurations. More substantial machines with an integrated stand are intended for workshops and production departments regularly processing shafts, bushes, flanges and components of varying size. Any more compact configurations can serve laboratories, education, prototyping and maintenance work on smaller parts. Mechanical feeds, digital readout, spindle-speed control, threading systems, coolant equipment, guards and accessories depend on the selected LTF model and must always be checked in its specification.
The bed is the machine’s principal geometric reference. Its guideways control carriage travel and the relationship between the headstock and tailstock. Bed mass, cross-section and rigidity affect the ability to absorb cutting forces and limit vibration. A rigid base supports the machine, provides a suitable working height and may incorporate storage, a chip tray or coolant collection where included. Even a heavily constructed lathe must be installed on an appropriate floor, accurately levelled and secured without twisting the bed.
The headstock contains the spindle assembly and transmission. On LTF geared-head configurations, ratios are selected to match spindle speed to workpiece diameter, material and operation. Other models may use different speed-changing systems or continuously variable control. Variable speed simplifies adjustment during changing cutting conditions, while defined mechanical ratios can provide effective torque delivery. The arrangement fitted to the individual LTF lathe must be confirmed before purchase.
A self-centring chuck provides rapid clamping of regular round, hexagonal and similar stock. Its jaws move together, but this does not guarantee zero runout, especially when gripping a previously machined surface. A dial-indicator check is advisable for close tolerances. An independent-jaw chuck allows each jaw to be adjusted separately and is suitable for irregular castings, eccentric parts and components that must be aligned accurately to a particular surface.
Jaws must be selected according to diameter, geometry and surface-protection requirements. Standard jaws are commonly used for external gripping within their working range. Reversed or external jaws can extend the gripping diameter or provide internal gripping when permitted by the chuck design. Soft jaws can be machined to the actual workpiece diameter, improving contact, concentricity and force distribution. Shaped jaws are particularly useful for thin, finished, irregular or easily distorted components.
The workpiece must enter the chuck deeply enough to provide secure support, and projection should be limited to the minimum required for access. Excessive projection creates leverage, increases chuck loading and allows the part to deflect under cutting force. Chatter, unintended taper, dimensional error, poor finish or loss of grip can result. Increasing jaw pressure cannot compensate for unsuitable engagement geometry and may distort the component.
Long or slender workpieces require support from the tailstock, a fixed steady or a travelling steady. The tailstock supports the free end with a dead or live centre. A fixed steady is locked to the bed and supports the part at a chosen position, while a travelling steady moves with the carriage and supports the workpiece close to the cutting zone. Pads or rollers must be set uniformly without preventing rotation or forcing the component away from the spindle axis. Contact points require cleaning and, where specified, lubrication.
Turning between centres is appropriate for shafts and components that must preserve a common axis after removal and remounting. Centre holes must be properly prepared, centres must be clean and aligned, and an appropriate drive system must transmit rotation. Tailstock pressure should support the workpiece without overloading the centres or bending a slender part. Thermal expansion and settling should be monitored because they can change the supporting condition during machining.
Collets are suitable for regular bar stock and smaller parts when concentricity, rapid changeover and minimal surface marking are important. The collet, mounting and closer must be compatible with the LTF lathe. A collet must remain within its specified gripping range; clamping an unsuitable diameter produces irregular contact, reduces concentricity and can damage the system.
Bars passing through the spindle bore must be supported and guarded behind the headstock. A long unsupported section can bend and rotate violently. Suitable bar guides, supports or containment devices must be used and access to the area prevented. Spindle bore is therefore a major selection criterion, but it must be considered together with stock length and the ability to contain the projecting portion safely.
Before starting, the operator must verify workpiece and tool clamping, remove the chuck key and check all control positions. A preliminary manual rotation, performed under the conditions specified by the manufacturer, confirms that the jaws, workpiece, cutting tool, tool post, tailstock and steadies cannot collide. This is particularly important with reversed jaws, eccentric work, long tools and operations close to the chuck.
The cutting edge should normally be set at spindle centre height. An edge positioned too high or too low changes effective tool geometry, modifies cutting forces and may leave a central pip during facing. Tool projection from the holder must be restricted to the length required for access. The holder must have adequate cross-section and seat on clean, undamaged tool-post surfaces.
High-speed-steel tools are resharpenable and can provide keen or customised cutting geometries. They are useful for controlled cuts, softer materials, form tools and work where cutting speed is not the primary productivity factor. Solid or brazed carbide tools provide greater wear resistance. Indexable tooling allows rapid cutting-edge replacement and the selection of grades and geometries for steel, stainless steel, cast iron, aluminium, copper, brass, bronze, engineering plastics and other compatible materials.
Roughing requires a robust cutting edge, reliable chip control and the capacity to withstand feeds and depths of cut consistent with system rigidity. Semi-finishing balances productivity and surface quality. Finishing uses geometries suitable for lighter cuts while maintaining sufficient engagement to prevent rubbing. A nominal finishing insert cannot produce a good surface if the machine chatters, the part deflects or the edge operates outside its intended range.
The chipbreaker must be chosen according to material, feed and depth of cut. If chip flow does not reach the intended breaker geometry, chips can remain long and continuous; if loading is excessive, the insert can chip. Nose radius affects edge strength, roughness and radial cutting force. A larger radius may improve finish and support higher feed but requires greater rigidity. A smaller radius reduces lateral force and suits slender parts and detailed profiles but provides a less robust edge.
Spindle speed is selected from the cutting speed required by the workpiece material and tool and from the actual machining diameter. As diameter increases, spindle speed normally has to decrease to maintain an appropriate surface speed. During facing, the cutting diameter decreases as the tool approaches the centre. Continuously variable control, where fitted to an LTF model, facilitates adaptation but does not replace correct parameter selection or the operating limits of tool, chuck and workpiece.
Feed determines tool travel per spindle revolution and affects productivity, surface finish and chip formation. Depth of cut determines the amount removed radially. The two parameters must be considered together. Excessive loading can cause deflection, chatter, overload and rapid wear; insufficient engagement can cause rubbing, work hardening and poor chip control. A trial pass should be made before reaching the final size, with a suitable machining allowance retained for finishing.
The saddle travels longitudinally along the bed. It carries the cross slide, which moves the tool radially, and the swivelling compound slide, which provides fine adjustment and inclined movement. Mechanical longitudinal and cross feeds, where fitted to the selected LTF lathe, improve travel uniformity and surface quality compared with exclusive hand feeding. Feed direction, available ranges and engagement systems depend on the specific configuration.
The swivelling compound can produce relatively short tapers by being set to the required angle and advanced along that direction. Shallow tapers on work held between centres may sometimes be produced by controlled tailstock offset; some models can accept dedicated taper-turning equipment. Tailstock displacement changes machine alignment and must be restored and verified before normal cylindrical turning resumes.
Thread cutting synchronises spindle rotation with longitudinal carriage movement. The leadscrew provides the fixed relationship required to generate the selected pitch, while the feed shaft is generally used for normal powered feeds. Change gears, selector levers and gearbox settings must be arranged exactly as specified for the LTF lathe.
Before threading, the operator must verify pitch, thread form, right- or left-hand direction, starting diameter, tool alignment and run-out clearance. The tool must be set at spindle centre height and aligned correctly with the workpiece. A relief groove can provide space to complete the pass before a shoulder. Initial cuts should be light, and the pitch should only be checked with a gauge or suitable measuring system after the spindle has stopped.
The tailstock supports the workpiece and carries drill chucks or taper-shank tooling. It can be used for centre drilling, drilling, countersinking, reaming and controlled tapping where machine and procedure permit. The tool must seat correctly in the taper and quill extension should be restricted to the necessary length. Excessive extension reduces rigidity.
Tailstock alignment with the spindle axis must be checked periodically. Lateral or vertical error can cause taper in supported work, off-centre holes and uneven centre loading. A test bar, dial indicator or other appropriate metrological method can be used. After adjustment, a trial component or test cut should confirm the result.
Drilling requires accurate centre preparation and controlled quill feed. For deep holes, the drill must be withdrawn periodically to clear chips and renew lubrication. Long flexible drills can wander, so short rigid tooling should be used wherever possible. Internal boring with a tool held in the tool post requires a bar of adequate diameter and minimum practical projection. An excessively long boring bar can vibrate and produce tapered or scored surfaces.
Knurling forms a pattern by plastic displacement rather than conventional chip removal. Radial forces can be substantial, so the workpiece must be supported and the knurling holder correctly aligned. Wheel pitch and geometry must suit the component diameter to avoid double tracking. Controlled engagement, steady feed and appropriate lubrication help produce a uniform pattern.
Dial indicators, test indicators, micrometers, callipers, bore gauges, depth gauges and thread gauges are used to check runout, diameters, lengths, shoulders, grooves and geometry. Measurement must only be performed with the spindle completely stopped. A digital readout, where fitted to an LTF lathe, simplifies slide-position control, reduces handwheel-counting errors and supports repeatability. It does not directly measure the finished component and does not replace final metrological inspection.
Backlash between feed screws and nuts must be considered whenever movement is reversed. For repeatable positioning, the target should generally be approached from the same direction. Saddle, cross-slide and compound gibs can be adjusted progressively to reduce clearance without restricting smooth travel. Excessive tightening increases wear and produces irregular movement; excessive looseness encourages chatter and dimensional variation.
Coolant helps control heat and friction, supports chip evacuation and can improve tool life and surface finish. It must be selected according to material, cutting tool and operation. Some inserts are intended for dry machining, whereas drilling, threading, tapping, reaming and tough materials may require continuous or localised lubrication. Coolant must reach the cutting zone effectively, and intermittent application should be avoided where it could thermally shock the edge.
Chip shape, colour, length and consistency help the operator assess the process. Long chips may wrap around the component or tool, while unusual colour or fragmentation may indicate heat, wear or unsuitable parameters. Chips must never be removed by hand while the spindle is rotating. After the LTF lathe has stopped, a brush, chip hook or dedicated tool must be used while protecting the hands from sharp edges.
Routine maintenance of LTF precision centre lathes includes cleaning the bedways and machined surfaces, removing chips, lubricating guides, screws and all points specified by the manufacturer and checking lubricant level and condition. Precision surfaces should be protected against corrosion. The chuck and jaws should be cleaned periodically without allowing chips to enter their guides and internal clamping mechanisms.
Belts, gears and transmissions, where present, must be checked for tension, wear, lubrication and unusual noise. Saddle, cross-slide and compound clearances, headstock-to-tailstock alignment, pumps, guards, switches and emergency-stop functions also require inspection. Adjustment, maintenance, tool replacement and accessory changes must only be performed with the machine stopped and made safe.
Eye protection and close-fitting clothing are required during operation. Long hair must be secured. Gloves, jewellery, loose sleeves and anything that can be caught by rotating parts must not be worn near the working area. The rotating workpiece, chuck and chips must not be touched. Measurements must never be taken during rotation, and the chuck must not be slowed by hand.
The guards provided on an LTF lathe must remain closed and correctly positioned. The workpiece and cutting tool must be securely clamped before start-up. Long bars require support and containment behind the spindle. Tools must not be left on the bed, and the workplace must remain clean, organised and adequately illuminated. Unusual noise, vibration or behaviour requires an immediate stop and investigation.
Selecting an LTF precision lathe requires consideration of spindle bore, distance and height between centres, usable swing in the different machine areas, bed construction, spindle-speed range and control system, available feeds, threading capability, slide travels, spindle mounting, headstock and tailstock tapers, power, electrical supply, digital readout, coolant system, guards, stand and accessory compatibility. Maximum capacities alone do not define the machine’s practical suitability.
The decision should begin with the components machined most frequently, considering diameter, length, mass, material, tolerance, finish, workholding and duty cycle. Selecting solely for a rare maximum-size component may result in unnecessary cost and footprint. A machine that is too small for routine work may restrict rigidity, accuracy, productivity and service life. Space must also be allowed for chuck, tailstock, steadies, tooling and safe component handling.
LTF precision centre lathes are used in mechanical workshops, toolrooms, machine building, industrial maintenance, automotive work, production departments, laboratories and vocational education. They support one-off components, prototypes and small batches as well as repairs, adaptation and reconstruction of obsolete parts such as shafts, pins, bushes, flanges, spacers, fittings, pulleys, hubs and specialised tooling.
Tadaah supplies LTF precision centre lathes and assists customers in selecting a configuration consistent with their components, tolerances, materials, operating frequency and required accessories. Tadaah’s technical support concerns the correct selection and sale of the machine and does not imply that Tadaah provides turning services. Capacities, equipment, feeds, controls and accessory compatibility must always be confirmed in the specification of the individual LTF model.